
Drying Oven Airflow, Moisture Exhaust & Ventilation
How circulation airflow, moisture exhaust, fresh-air make-up, chamber pressure, humidity loading, and vent placement work together in an industrial drying oven—and how to avoid the common mistake of treating exhaust and circulation as the same system.
- Circulation and exhaust do different jobs. Circulation moves heat through the load; exhaust removes moisture or vapor from the oven atmosphere.
- Exhaust should follow the actual moisture or vapor load. A generic “air changes per hour” value is usually not enough to define drying performance.
- More exhaust is not automatically better. Excessive exhaust increases heater load, can pull in cold air, and may destabilize temperature and airflow.
- Vent location matters. Supply, return, exhaust, and make-up-air placement should prevent short-circuit airflow and force useful air movement through the product.
Circulation, Exhaust, and Make-Up Air Are Three Different Functions
Drying performance depends on how these three functions interact. They should be designed together, but they should not be confused with one another.
Circulation Air
Recirculates hot air through the chamber and product load to transfer heat and reduce local temperature differences.
Exhaust Air
Removes humid air, vapor, or process emissions from the oven so the gas phase does not become saturated or unstable.
Make-Up Air
Replaces the air removed by exhaust and helps control chamber pressure, but it also creates an additional heating load.
Start with What the Oven Must Remove from the Product
Exhaust should be linked to the actual drying load. That means estimating how much water, solvent, or other volatile material leaves the product per batch or per hour—and when that release occurs during the process.
- Incoming product moisture or volatile content
- Target final moisture or process condition
- Batch quantity or hourly production rate
- Whether release is steady or peaks during heat-up
- Whether the released material is water vapor or a flammable / hazardous volatile
Example
If one batch removes 30 kg of water over a 2-hour drying period, the average moisture-removal rate is:
The actual peak may be higher if most evaporation occurs early in the cycle. Exhaust and heat-load calculations should account for the real release profile where possible.
Select Circulation Airflow Around the Product and Loading Pattern
Drying slows when hot air travels around the load instead of through it. Fan size alone does not solve this problem. The supply and return arrangement must force useful air movement across the wet surfaces and through the loaded volume.
Horizontal Flow
Often useful for racks, carts, tray stacks, and loads where air should pass across product layers.
Vertical Flow
Useful where product geometry or conveyor support favors top-down or bottom-up air movement.
Side Supply / Return
Can provide controlled crossflow when chambers are wide or when multiple carts must receive similar airflow.
Custom Ducted Flow
Useful for complex shapes, dense loading, deep chambers, or applications requiring localized high-velocity air.
- Leave free-air passages between trays, shelves, products, and chamber walls
- Avoid placing large solid surfaces directly in front of supply or return openings
- Check the first and last rows of product, not only the center of the load
- Use baffles or ducting when the chamber geometry creates obvious bypass paths
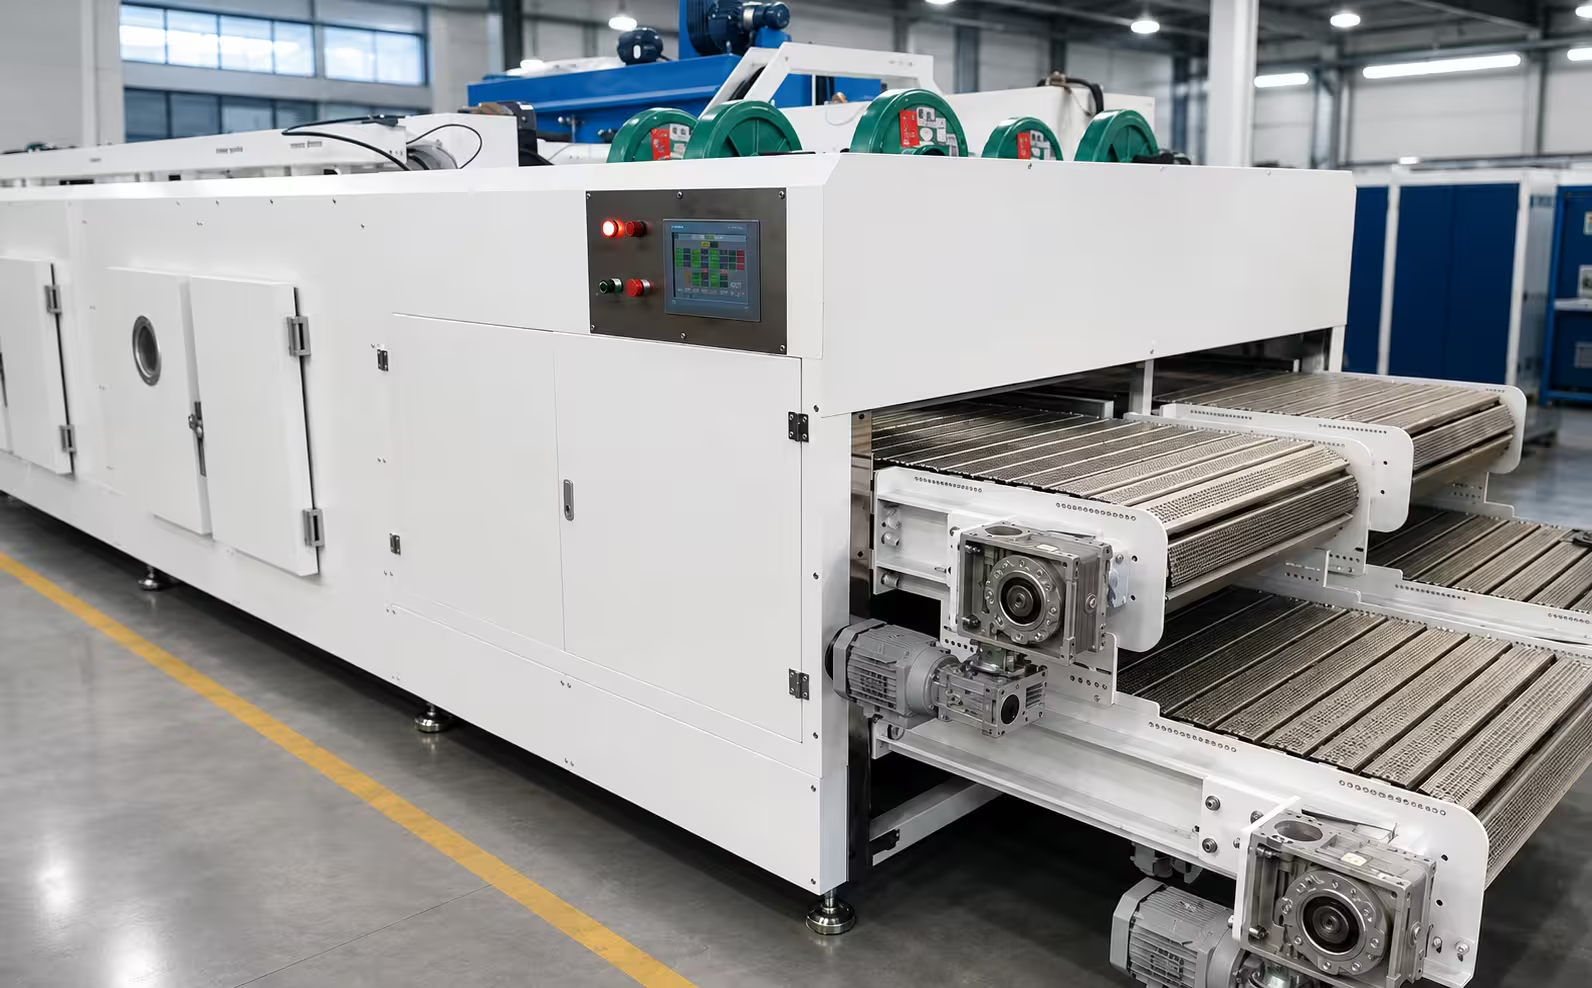
For equipment centered on strong convective drying, see Hot Air Circulation Dryers.
Estimate Exhaust from the Moisture-Carrying Capacity of the Air
One useful engineering approach is to treat the oven as a moisture mass-balance problem. The exhaust stream must carry away the water that leaves the product.
This relationship shows why exhaust cannot be defined by oven volume alone. The required airflow depends on how much moisture must be carried away and how much humidity increase the process can tolerate between inlet and exhaust air.
Balance Exhaust with Make-Up Air and Chamber Pressure
Every kilogram of exhaust air leaving the oven must ultimately be replaced by air entering the system. If make-up air is uncontrolled, the oven can pull cold air through doors, conveyor openings, seals, or gaps and disturb the thermal process.
Slight Negative Pressure
Often used where it is desirable to keep moisture or process vapor from leaking into the surrounding plant.
Near-Neutral Pressure
Useful where uncontrolled infiltration must be minimized and stable temperature is a priority.
Controlled Make-Up Air
Allows incoming air to enter at a defined location rather than through random gaps and openings.
Place Supply, Return, Exhaust, and Make-Up Air to Avoid Short-Circuit Flow
A poor vent layout can move air from inlet to exhaust without meaningfully passing through the product. The goal is to create a useful flow path through the loaded chamber before humid air leaves the oven.
- Do not place make-up air directly beside the exhaust unless the process intentionally requires it
- Locate exhaust where humid or vapor-laden air actually accumulates or exits the load
- Keep supply and return paths balanced across the chamber
- For deep or long chambers, consider multiple supply or return zones
- For conveyor systems, evaluate zone-to-zone leakage through product openings
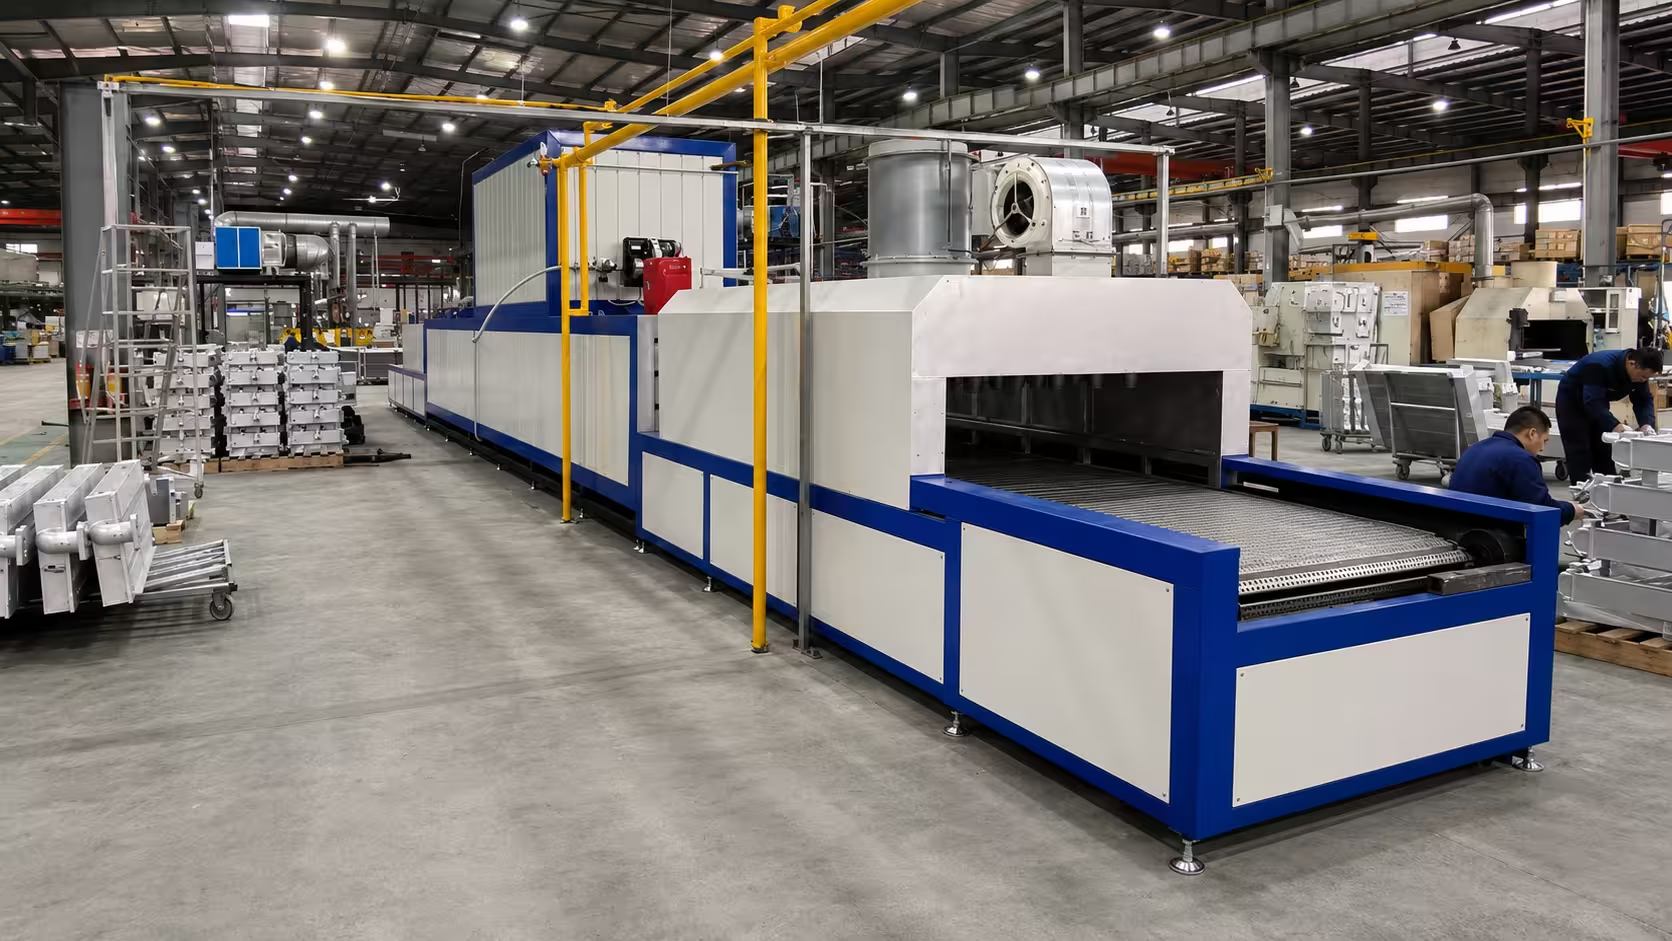
Batch and Continuous Dryers Need Different Ventilation Strategies
The moisture-release pattern and pressure behavior differ significantly between a closed batch chamber and a conveyor dryer with permanent inlet and outlet openings.
| Design Area | Batch Drying Oven | Continuous Conveyor Dryer |
|---|---|---|
| Moisture release | Often peaks after loading / heat-up | Often linked to hourly throughput and zone position |
| Air leakage | Primarily doors, seals, intentional vents | Continuous infiltration / exfiltration at conveyor openings |
| Exhaust control | Can be constant or staged through the batch cycle | May be zone-specific and coordinated with line speed |
| Pressure control | Usually easier to stabilize after doors close | Must account for continuous open product passages |
| Process zoning | Usually one chamber or limited zones | Can use flash-off, drying, final dry, and cooling zones |
For generic continuous drying equipment, see Industrial Conveyor Belt Dryer. Where linear plant space is limited, see U-Shaped Drying Oven.
Drying Rate Depends on Both Thermal Energy and the Moisture Capacity of the Air
Warmer air can generally carry more water vapor, but temperature alone does not guarantee fast drying. Drying slows if the air near the product becomes saturated, if circulation is weak, or if moisture cannot leave the product internally.
Temperature
Raises vapor pressure and can increase evaporation rate, subject to product limits and material behavior.
Air Velocity
Reduces the humid boundary layer at the product surface and improves convective heat and mass transfer.
Humidity Difference
A larger moisture-driving force between the product surface and the surrounding air generally supports faster drying.
Preliminary Moisture-Exhaust Calculation Example
This simplified example shows how a moisture mass balance can be used to estimate exhaust directionally. It is not a final fan or duct selection.
| Input | Example Value |
|---|---|
| Average water removal | 15 kg/h |
| Inlet humidity ratio, ω_in | 0.010 kg water / kg dry air |
| Target exhaust humidity ratio, ω_out | 0.030 kg water / kg dry air |
| Humidity-ratio increase | 0.020 kg/kg dry air |
If dry-air density at the relevant condition were approximately 1.0 kg/m³, this would correspond directionally to about 750 m³/h of dry-air flow. Actual volumetric airflow depends on temperature, pressure, humidity, leakage, required safety margin, and whether the moisture release peaks above the average.
More Exhaust Can Increase Energy Use and Make Temperature Control Worse
Exhaust is necessary for moisture removal, but excessive exhaust can make the oven harder to control. Every additional unit of air removed must be replaced and reheated.
Higher Heater Load
More fresh air must be heated from ambient temperature to the process setpoint.
Longer Heat-Up
If installed heating power is fixed, excessive exhaust can slow recovery and extend cycle time.
Cold-Air Infiltration
Strong negative pressure can pull cold air through doors, seals, or conveyor openings.
Poor Uniformity
Unbalanced exhaust or make-up air can create hot and cold regions even when circulation fans are adequate.
Use enough exhaust to remove the required moisture or vapor while preserving stable circulation, chamber pressure, temperature recovery, and energy efficiency.
Turn Airflow and Exhaust Requirements into an Oven Specification
A useful drying-oven RFQ should identify the product, loading pattern, incoming moisture or volatile content, required drying time, temperature, batch or hourly output, airflow concerns, exhaust route, utilities, controls, and any temperature-uniformity or FAT requirements.
Confirm Overall Sizing
Use How to Size an Industrial Drying Oven for chamber, moisture, heat-load, and heating-power relationships.
Prepare the RFQ
Use the Industrial Drying Oven RFQ Checklist to organize project data for quotation.
Review the Product Family
See Industrial Drying Ovens for batch, hot-air, high-temperature, infrared, conveyor, and custom drying equipment.
Drying Oven Airflow & Ventilation FAQ
What is the difference between circulation airflow and exhaust airflow in a drying oven?
How much exhaust does an industrial drying oven need?
Can too much exhaust reduce drying oven performance?
Where should the exhaust vent be located in a drying oven?
How does airflow direction affect drying time?
Should batch and conveyor drying ovens use the same ventilation design?
What information should I send for drying-oven airflow and exhaust design?