
Overhead Conveyor Oven
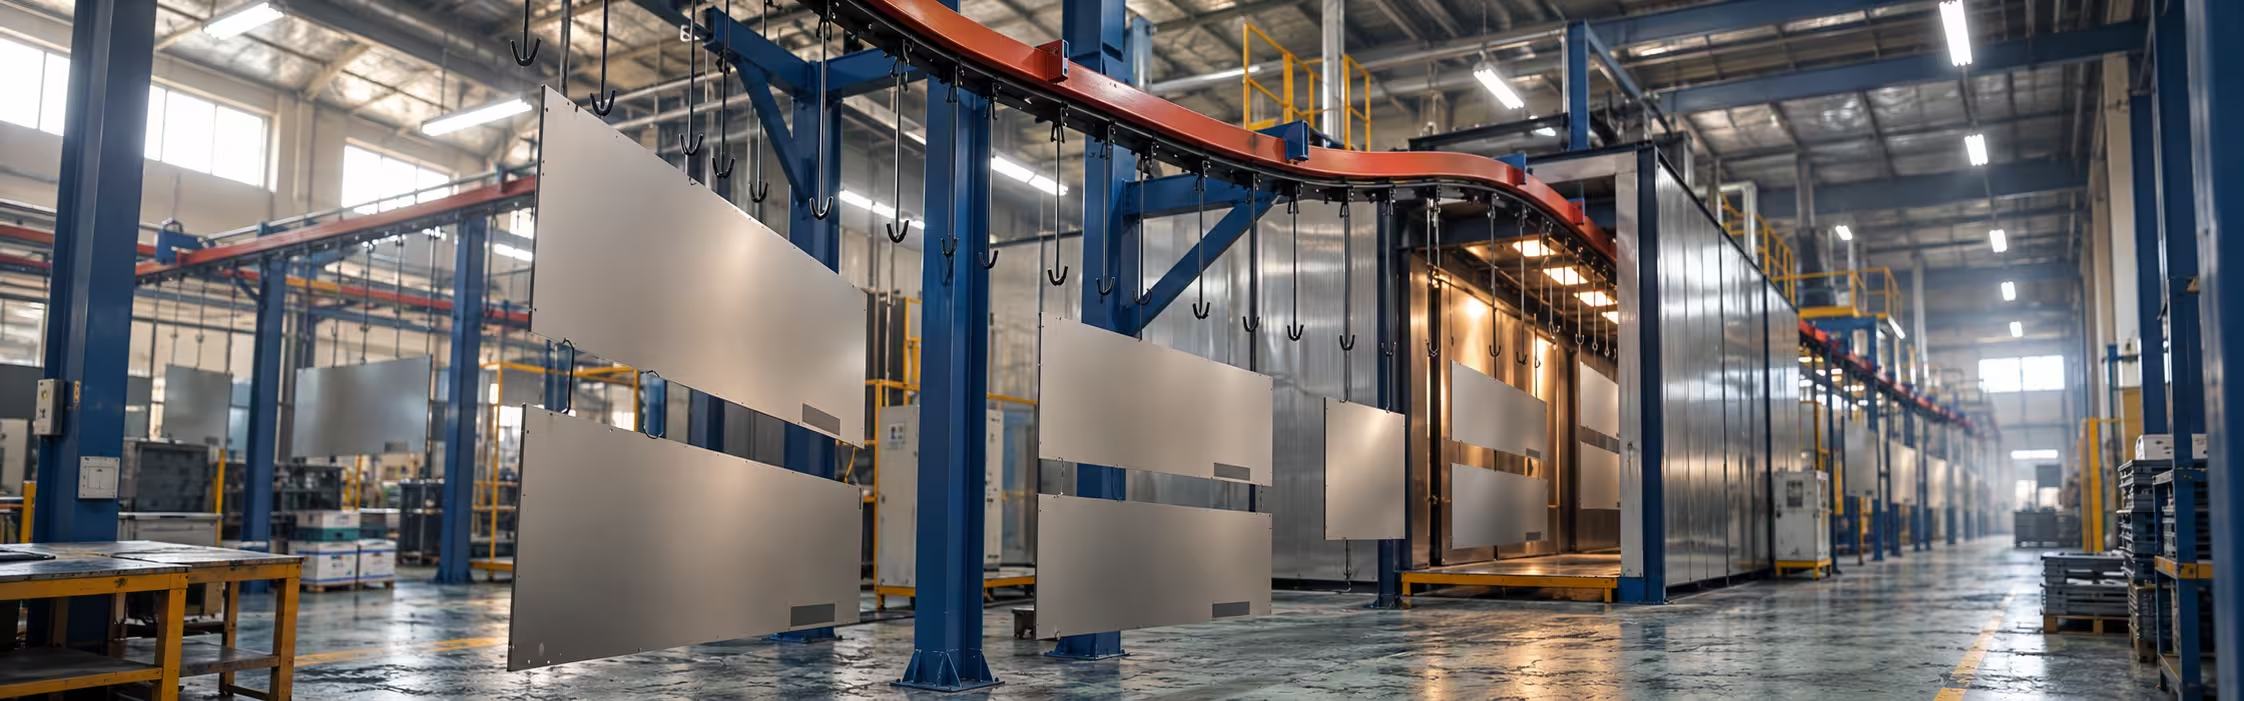
ZonHoo overhead conveyor ovens are designed for continuous lines where parts travel suspended from a monorail or overhead track. Hanger spacing, part swing, track openings and heat coverage are engineered together so coated or finished parts can move through the oven without occupying floor conveyor space.
Watch a ZonHoo overhead conveyor oven with suspended-part handling, monorail routing and continuous movement through the heated process.
What Makes a Conveyor Oven “Overhead”?
An overhead conveyor oven carries parts from an overhead track rather than on a floor-level belt. The suspended transport method changes both the mechanical layout and the thermal design because the hanger, part orientation and track pass-through become part of the oven opening.
- Parts remain suspended throughout the thermal process.
- Hanger pitch determines product spacing and practical throughput.
- Part swing and rotation must stay within the safe chamber envelope.
- Track openings at the oven entry and exit require controlled transition and sealing concepts.
- Airflow must heat the full hanging geometry rather than only a flat belt plane.
The Right Direction When the Product Must Stay Suspended
If the product can travel on a conventional belt, start with the belt-based industrial conveyor oven. If you are still comparing all continuous transport types, compare continuous oven configurations.
This page is specifically for overhead conveyor oven, monorail conveyor oven, hanger conveyor oven and related suspended-part projects where routing, floor clearance and coating-line integration drive the machine architecture.
Four Details That Decide Whether an Overhead Oven Runs Smoothly
Overhead projects are more sensitive to carrier geometry and line interfaces than standard flat-belt systems. These details should be fixed before the chamber opening and heated length are finalized.
Hanger spacing & load pitch
Carrier pitch controls product spacing, production rate and the minimum clearance needed between hanging parts.
Swing & rotation envelope
Part movement through curves, transitions and airflow must remain inside the safe chamber envelope without contact.
Track openings & seals
The overhead rail passes through the oven shell, so entry / exit geometry and sealing strategy affect heat loss and stability.
Heat coverage on hanging parts
Air delivery must reach all relevant surfaces despite shadows created by hangers, fixtures and closely spaced components.
Size the Oven Around Hanger Pitch, Line Speed and Part Envelope
The same thermal dwell time can produce very different machine layouts depending on hanger spacing, track routing and how many parts must pass the oven each hour.
Core RFQ Inputs for an Overhead Conveyor Oven
Use the Existing Engineering Guides
For the broader equipment decision, start with the industrial conveyor oven selection guide.
Once line speed and required process time are known, use the conveyor oven sizing guide to convert process time into practical heated length.
- Do not size the chamber from part dimensions alone.
- Include hanger, hook and swing allowance in the usable envelope.
- Confirm oven openings only after the track interface is fixed.
Control Heat Loss Without Restricting the Overhead Track
The track must enter and leave the oven freely, but every opening becomes a path for heat loss and uncontrolled air movement. Good overhead oven design balances clearance, sealing and stable recirculation.
| Design area | What must be checked | Why it matters |
|---|---|---|
| Track pass-through | Rail height, brackets, chain or trolley path and required service clearance | Sets the shape and size of the unavoidable oven opening. |
| Part entrance envelope | Maximum part width plus swing and fixture allowance | Prevents collision while keeping the opening no larger than necessary. |
| Air curtain / baffle concept | Transition geometry and recirculation direction near entry and exit | Helps reduce uncontrolled heat escape and profile disturbance. |
| Hanger shadowing | Fixture density and airflow access around the top and sides of the product | Improves heat coverage on complex hanging geometry. |
| Line interlocks | Conveyor run status, oven ready, fault and emergency stop logic | Keeps the thermal process coordinated with the overhead conveyor system. |
Overhead Conveyor Oven Applications
Overhead ovens are strongest in finishing lines where the part should stay suspended before, during and after thermal processing.
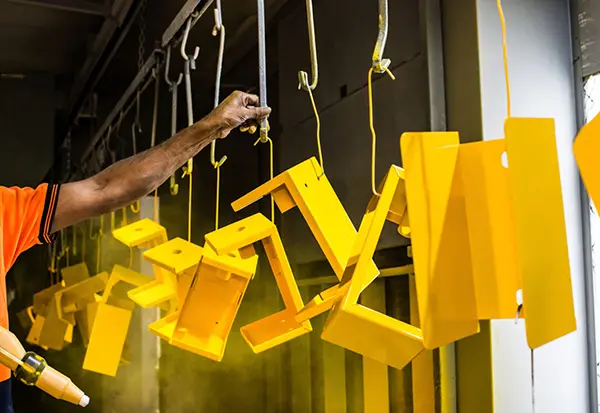
Continuous Coating & Curing
Suspended conveying keeps coated surfaces accessible and supports continuous flow through flash-off, drying or curing stages.
industrial ovens for coating processes →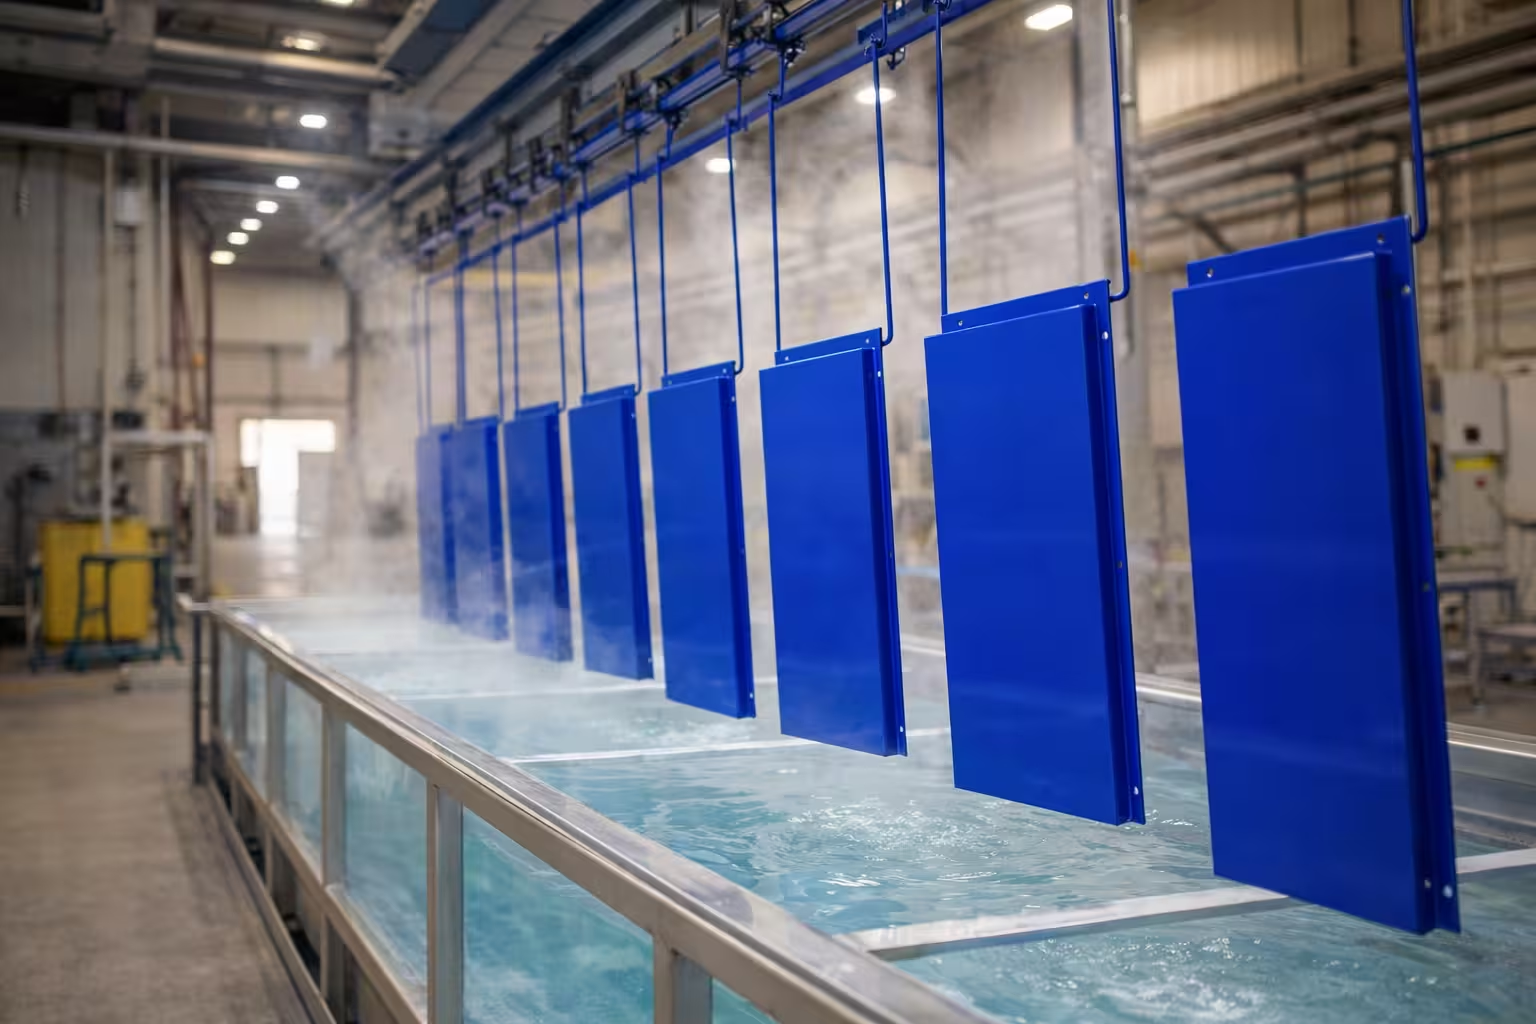
Pretreatment & Finishing Lines
Overhead routing works naturally with cleaning, pretreatment and finishing operations where floor access and part orientation matter.
surface-treatment conveyor heating →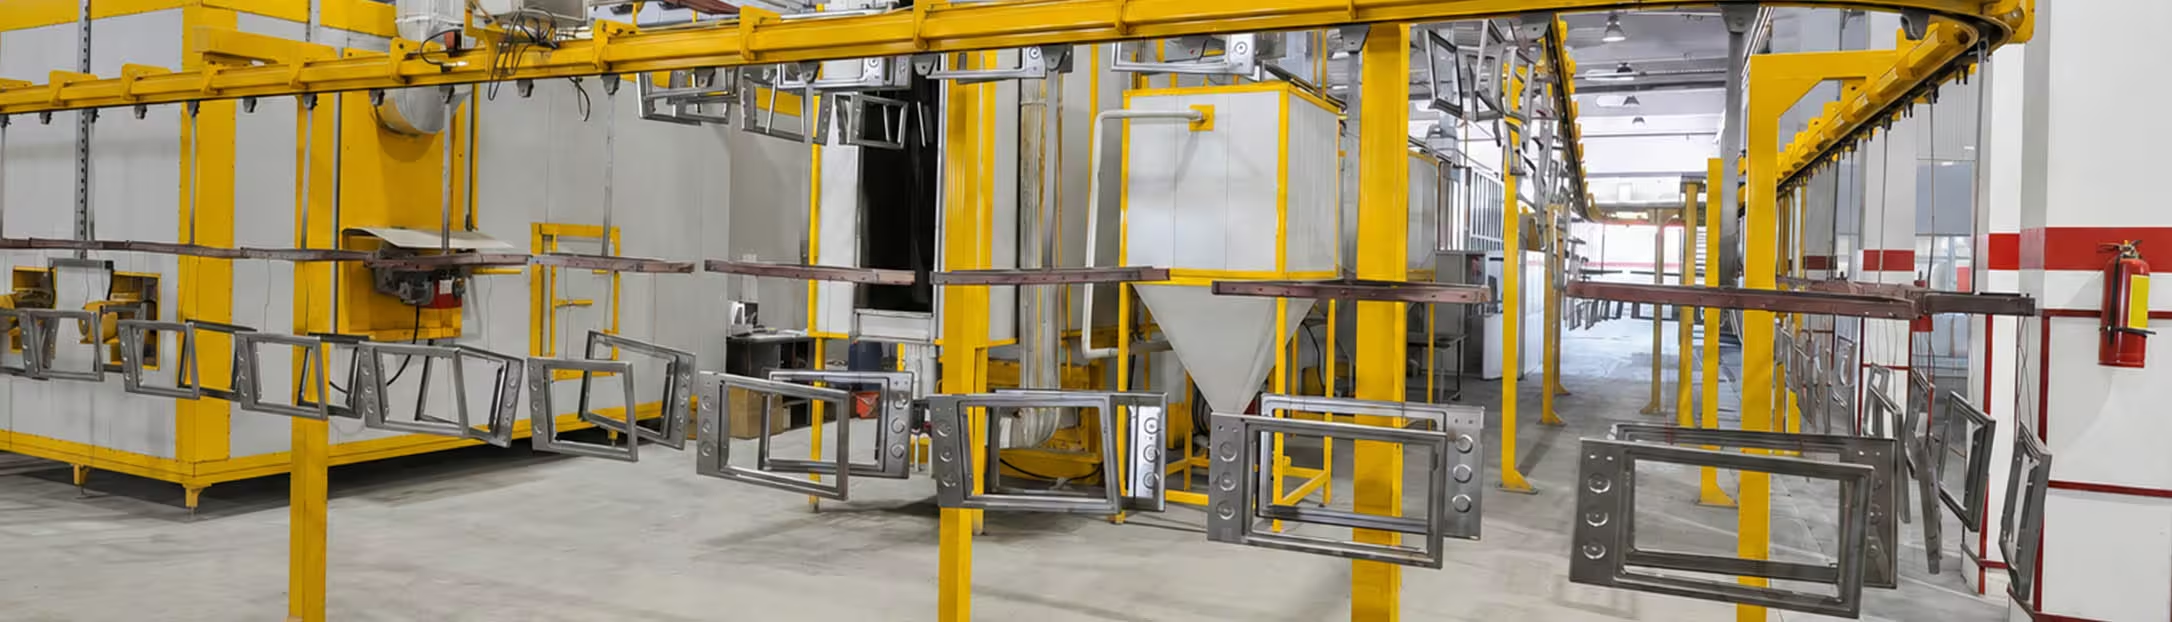
Powder Coating Cure
Hanging parts can move directly from application into the curing stage at controlled line speed for stable production rhythm.
powder coating oven applications →Coordinate the Oven with the Conveyor and Control System
An overhead curing oven should not be engineered as an isolated hot chamber. Track layout, controls, line status and process interlocks should be defined as one production system.
Oven System Planning
Coordinate line layout, track elevation, utilities, airflow, oven length and upstream / downstream equipment before fabrication.
industrial oven system planning →Industrial Oven Controls
Define recipes, alarms, conveyor run signals, ready / fault logic, temperature protection and production-line coordination.
industrial oven control systems →Build the Overhead Oven into the Complete Finishing Line
For many overhead projects, the oven is only one station in a larger coating system. The conveyor route, booth interfaces and curing capacity should be planned together.
Spray Coating & Curing Line
Combine surface preparation, spray application, overhead transport and thermal curing as one coordinated production flow.
integrated spray booth and curing oven line →Powder Coating Line
Plan conveyor routing, powder booth, curing residence time, line speed and unloading as one integrated system instead of separate equipment islands.
powder coating line →Overhead Conveyor Oven Questions
When should I choose an overhead conveyor oven instead of a belt conveyor oven?
Choose an overhead oven when parts should remain suspended, coated surfaces need open access, the floor must stay clear, or the production line already uses monorail or overhead conveyor handling.
How does hanger spacing affect oven capacity?
Hanger spacing controls how many carriers pass the oven per hour and how much clearance exists between products. It affects throughput, heat coverage and the practical line speed window.
Why is part swing important inside the oven?
Suspended parts can move because of conveyor transitions, airflow and product imbalance. The chamber opening and internal clearances should include a realistic swing allowance so parts do not contact the oven or each other.
How are overhead track openings sealed?
The exact solution depends on rail geometry and conveyor hardware. Typical design work focuses on keeping the pass-through as compact as practical and using baffles, transition sections or airflow management to limit heat loss without obstructing the conveyor.
Can an overhead conveyor oven be integrated directly with a powder coating line?
Yes. Overhead curing ovens are commonly engineered around coating-line conveyor routing, hanger pitch, booth interfaces, required cure time and line-speed coordination.